 English
 Español
 العربية

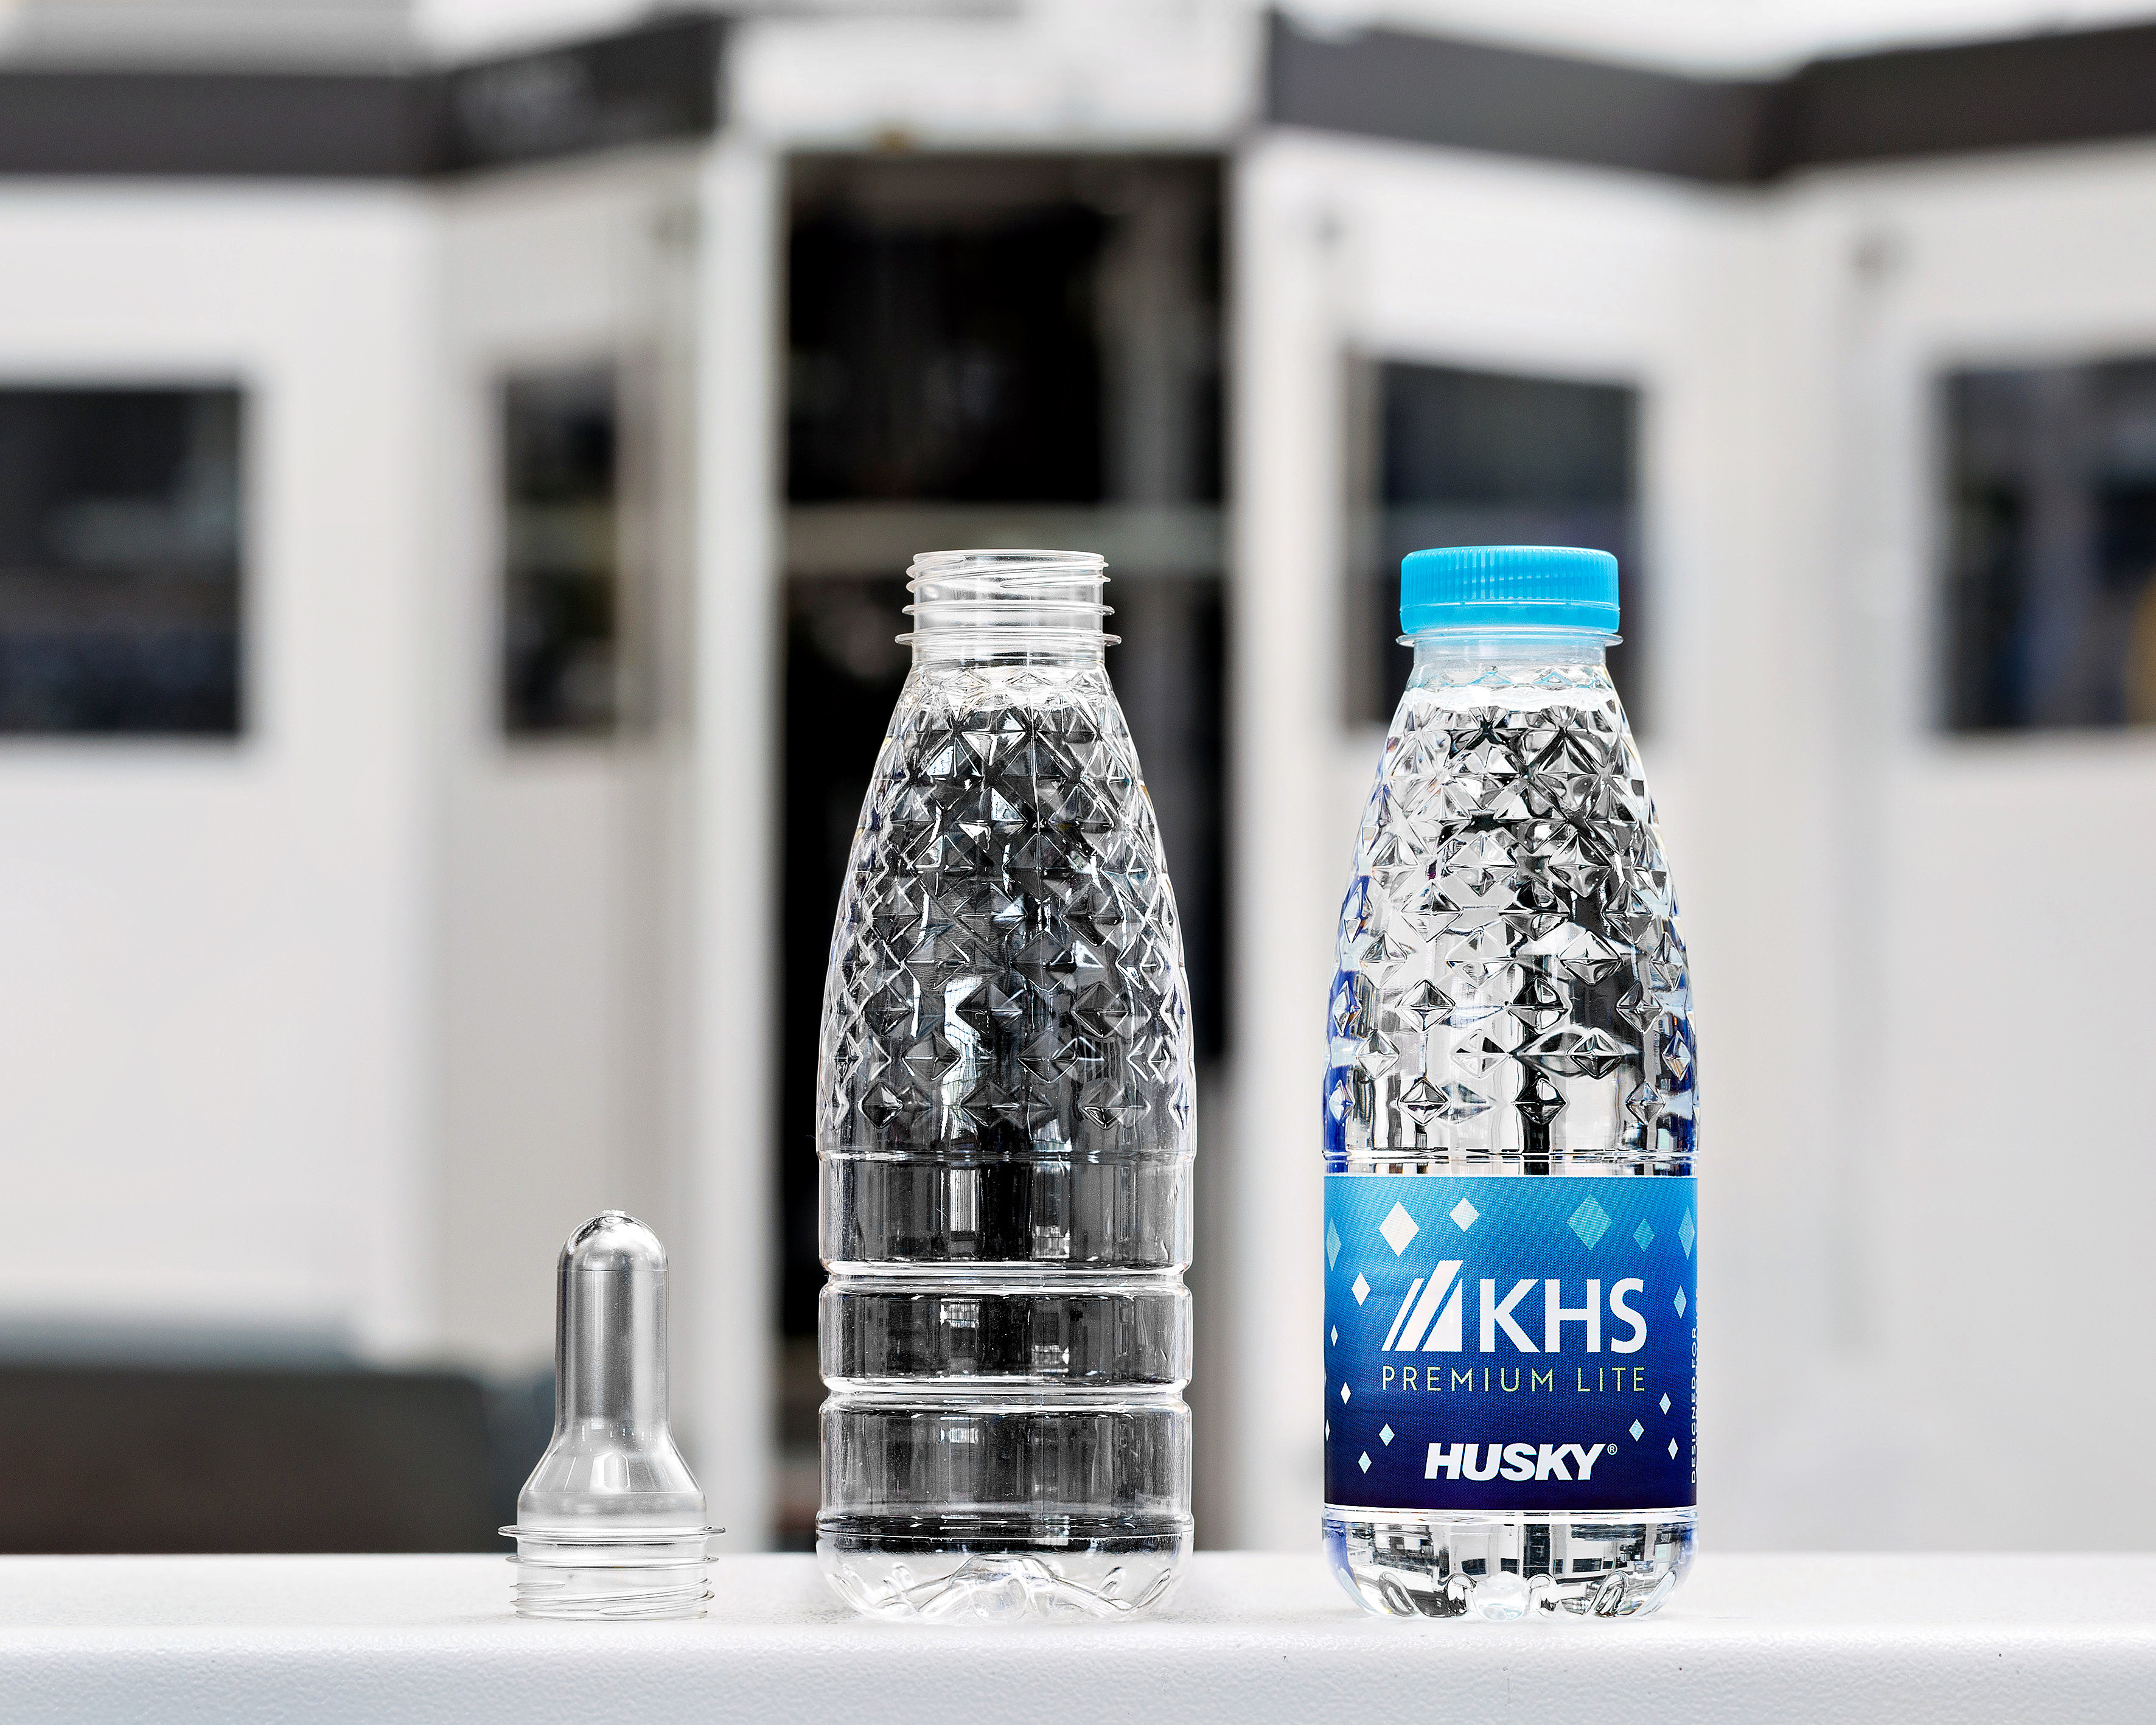
Many PET bottle factories experience a similar problem after upgrading to high-speed production:
At the beginning, production runs smoothly.
But after several months of continuous operation, problems gradually begin to appear:
increasing reject rates
unstable lightweight bottles
bottle deformation
random leakage problems
conveyor instability
higher compressed air consumption
inconsistent bottle dimensions
Many factories initially believe:
“The machine is getting old.”
However, after analyzing many PET production lines, we found that the real issue is often:
production system instability.
In modern PET manufacturing, stable production depends on much more than machine speed.
Especially during high-speed lightweight bottle production, even small engineering deviations become amplified over time.
One common hidden problem is:
cavity cooling imbalance.
When mold cooling efficiency differs between cavities:
bottle crystallization becomes inconsistent
wall thickness distribution changes
bottle rigidity becomes unstable
At lower production speeds, the effect may be small.
But during continuous high-speed operation, cavity cooling imbalance gradually increases reject rates and bottle instability.
Another major issue is:
air recovery instability.
Many factories focus heavily on blowing pressure itself, but ignore airflow recovery fluctuation.
When air recovery becomes unstable:
bottle expansion consistency decreases
stretching behavior changes
energy consumption increases
lightweight bottle deformation becomes more frequent
Over time, unstable airflow directly affects:
Stable PET Production.
We also frequently see:
neck finish tolerance problems.
Even very small neck dimension variation can create:
unstable cap sealing
transfer timing mismatch
leakage risk during transportation
filling line instability
This becomes even more serious during high-speed production where bottle transfer timing must remain extremely precise.
Another overlooked issue is:
top-load performance.
Many factories aggressively reduce bottle weight to save resin costs.
However, lightweight bottle optimization requires:
stable cooling
controlled crystallization
balanced wall thickness distribution
proper bottle structural support
Without full system coordination, lightweight bottles may lose top-load performance and become unstable during storage and transportation.
This is why modern PET factories increasingly focus on:
Mold-Machine Compatibility.
Because PET production stability depends on coordination between:
✔ PET blow molding machine
✔ PET preform mold
✔ cap mold
✔ airflow recovery system
✔ cooling balance
✔ bottle structure design
✔ transfer timing control
—not only machine speed.
At BANGEMACHINE, we focus on:
Stable PET Production
Lightweight Bottle Optimization
Mold-Machine Compatibility
PET Troubleshooting
Energy Saving
High-Speed PET Production
Because in real factory environments:
small engineering deviations create big long-term production losses.
Factories that focus only on maximum BPH often struggle with:
unstable production
higher maintenance cost
reject rate growth
energy waste
But factories that focus on system coordination achieve:
✔ lower reject rates
✔ stable bottle quality
✔ lower air consumption
✔ better lightweight bottle performance
✔ long-term production efficiency
In PET manufacturing: