 English
 Español
 العربية

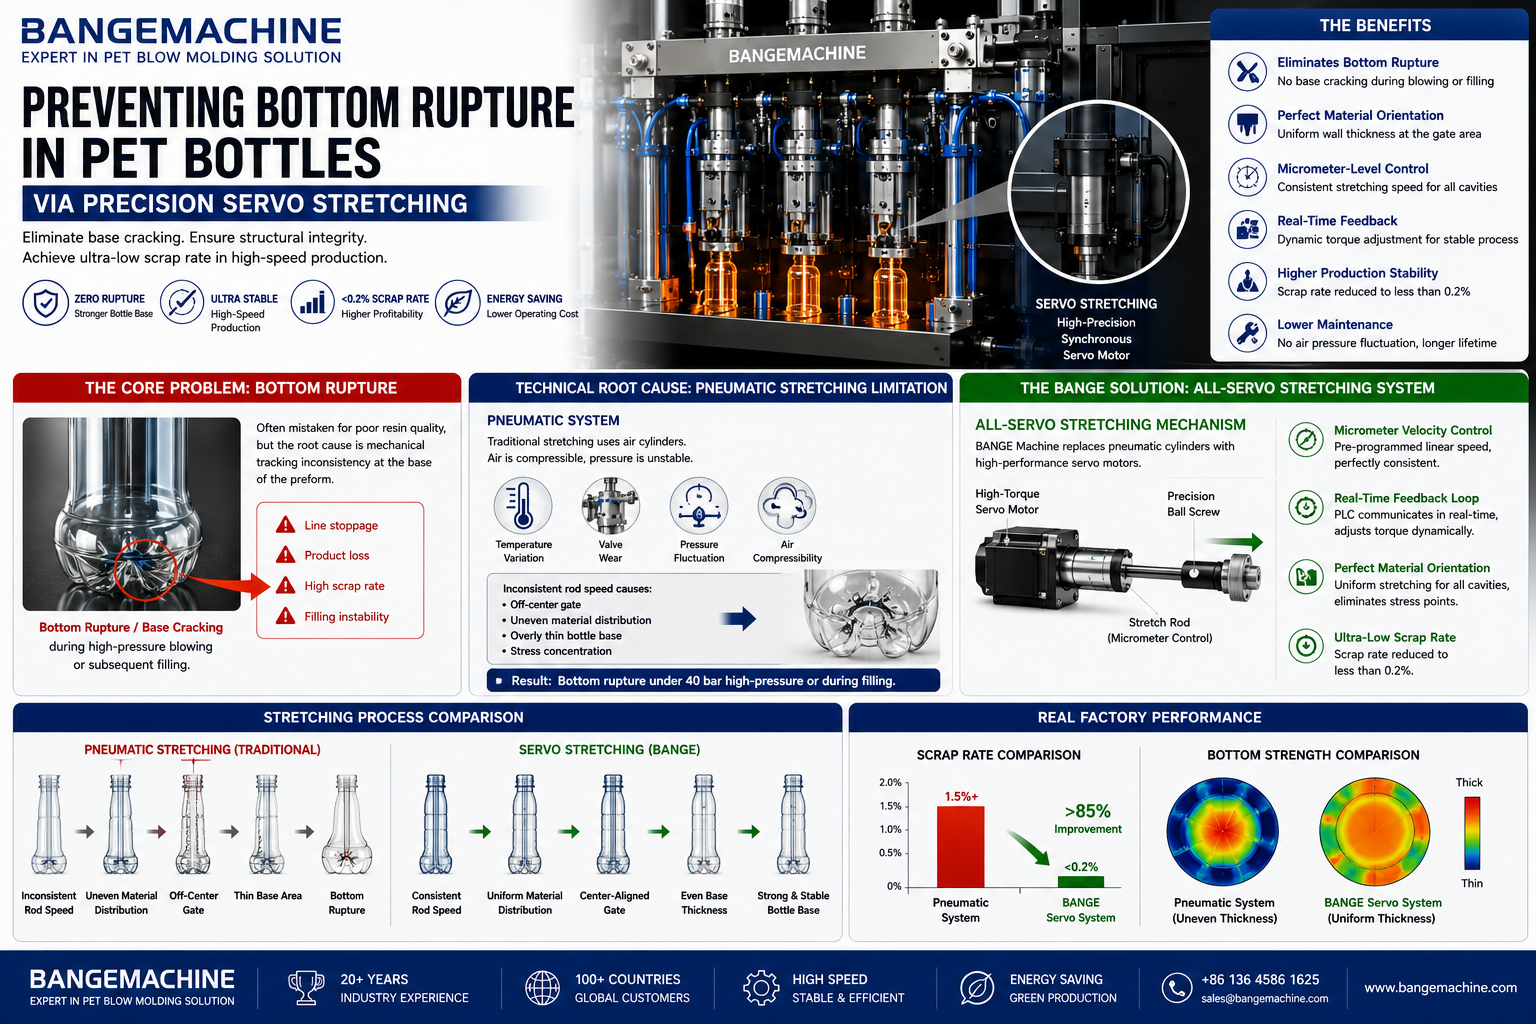
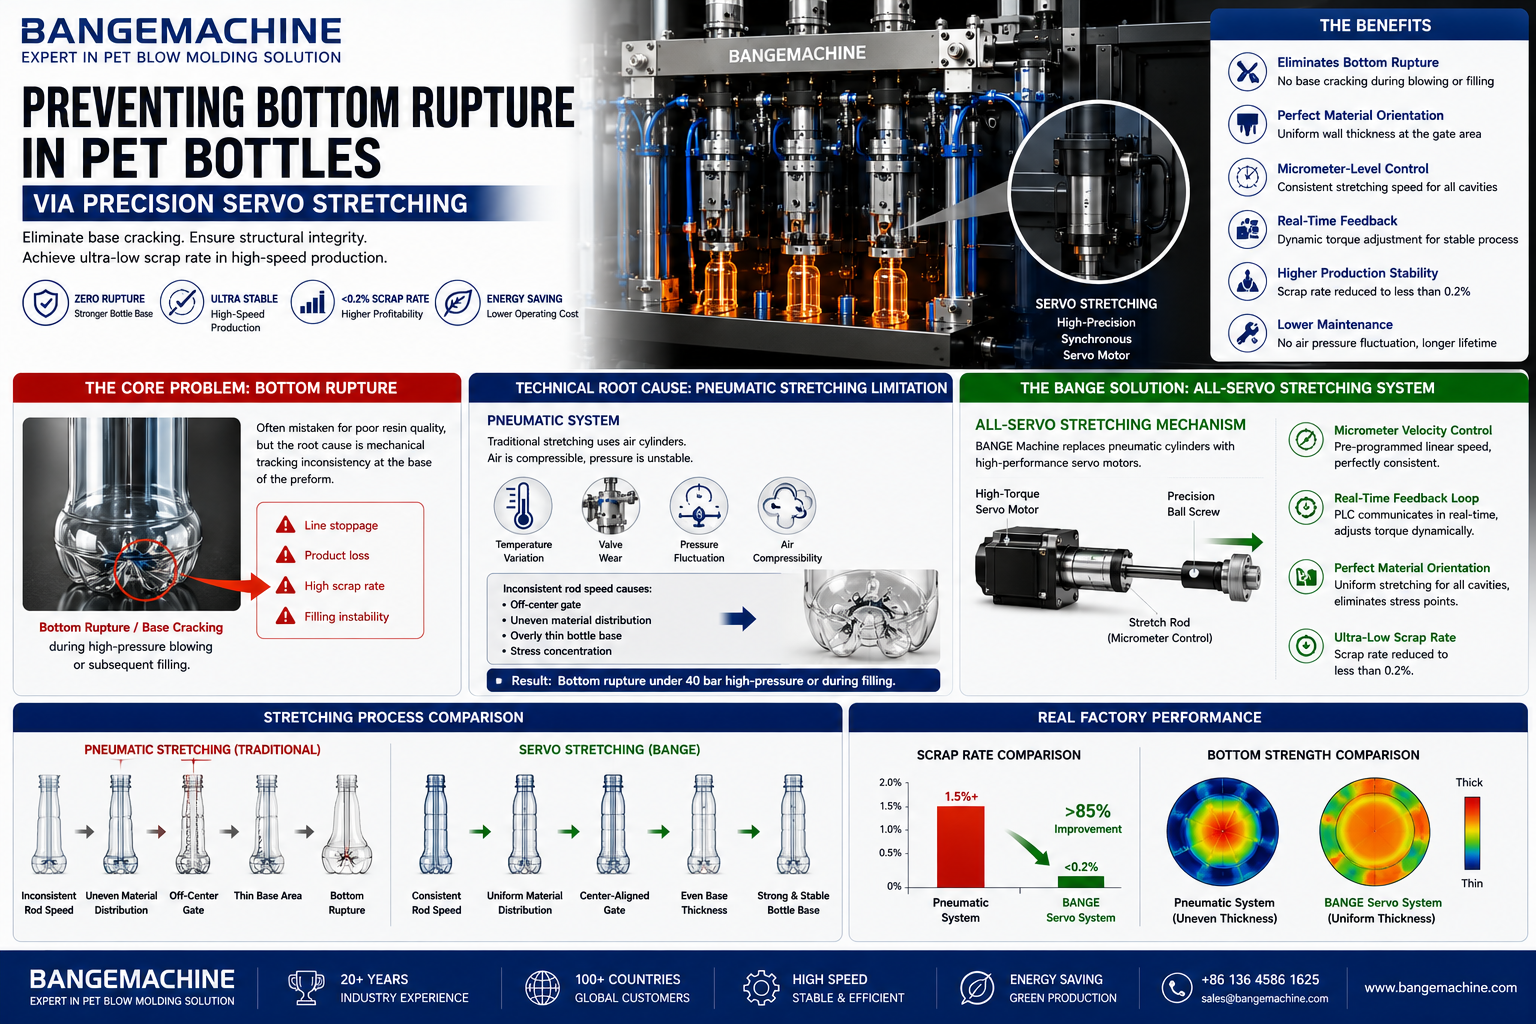
Bottom rupture is one of the most expensive defects in PET bottle production.
When the bottle base cracks during blowing or filling, factories face:
LINE STOPPAGE
PRODUCT LOSS
HIGHER SCRAP RATE
FILLING INSTABILITY
Many manufacturers blame resin quality.
But in most cases:
THE REAL PROBLEM IS STRETCHING INSTABILITY.
WHY BOTTOM RUPTURE HAPPENS
Traditional PET blow molding machines use pneumatic cylinders to drive the stretch rod.
The problem?
AIR PRESSURE IS NEVER COMPLETELY STABLE.
Pressure changes caused by:
- Ambient temperature
- Valve wear
- Compressor fluctuation
- Air recovery instability
can affect stretch rod movement.
When stretching speed becomes inconsistent:
- PET material distribution shifts
- The gate area becomes off-center
- The bottle base becomes too thin
Result:
STRESS CONCENTRATION AT THE BASE
WEAKER MATERIAL ORIENTATION
HIGHER RISK OF BOTTOM CRACKING
Especially during:
40 BAR HIGH-PRESSURE BLOWING
LIGHTWEIGHT BOTTLE PRODUCTION
HIGH-SPEED MULTI-CAVITY OPERATION
THE LIMITATION OF PNEUMATIC STRETCHING
Pneumatic systems cannot fully guarantee:
IDENTICAL STRETCHING SPEED
PERFECT CENTERLINE MOVEMENT
STABLE MATERIAL ORIENTATION
Even tiny movement variation between cavities can create:
- Uneven wall thickness distribution
- Base instability
- Gate eccentricity
- Crystallization imbalance
At high speed, these small differences become amplified.
THE BANGEMACHINE SERVO STRETCHING SOLUTION
BANGEMACHINE replaces pneumatic cylinders with:
FULL-SERVO STRETCH CONTROL
This creates far more stable and repeatable stretching behavior.
MICROMETER-LEVEL VELOCITY CONTROL
The stretch rod is driven by a high-torque synchronous servo motor.
Its movement profile is fully programmable.
Meaning:
PERFECTLY LINEAR STRETCHING SPEED
STABLE MATERIAL DISTRIBUTION
HIGHER BASE STRUCTURAL STRENGTH
Regardless of:
- Temperature changes
- Air pressure fluctuation
- Continuous production load
REAL-TIME PLC FEEDBACK CONTROL
The servo drive communicates continuously with the PLC system.
If resistance changes inside the PET preform:
TORQUE IS ADJUSTED IN REAL TIME
This ensures:
STABLE STRETCH SYNCHRONIZATION
IDENTICAL CAVITY PERFORMANCE
LOWER PROCESS DRIFT
WHY THIS MATTERS FOR LIGHTWEIGHT BOTTLES
Lightweight bottles have thinner material distribution.
Meaning:
THE BASE AREA BECOMES MUCH MORE SENSITIVE TO STRETCHING ERROR.
Servo stretching helps maintain:
UNIFORM GATE THICKNESS
STABLE BASE ORIENTATION
LOWER STRESS CONCENTRATION
BETTER BURST RESISTANCE
Result:
SCRAP RATE BELOW 0.2%
MORE STABLE FILLING PERFORMANCE